Welcome To Shijiazhuang Yongda Pump Co., Ltd.

Mud slurry pump guide: how to choose, use, and maintain the right pump for your project
Sep 20,2026
Author:
Yongda Pump

Article overview
This guide explains what a mud slurry pump is, how to select the right type for your application, and how to maintain it for maximum service life. It is written for engineers and procurement managers in Indonesia's mining, construction, and dredging sectors.
Table of contents
- 1. What is a mud slurry pump?
- 2. Main types of mud slurry pumps compared
- 3. How to choose the right mud slurry pump for your project
- 4. Key technical specifications explained
- 5. How to install and operate a mud slurry pump correctly
- 6. Maintenance best practices to extend pump life
- 7. 2026 trends: smart monitoring and advanced wear materials
- 8. FAQ
What is a mud slurry pump?
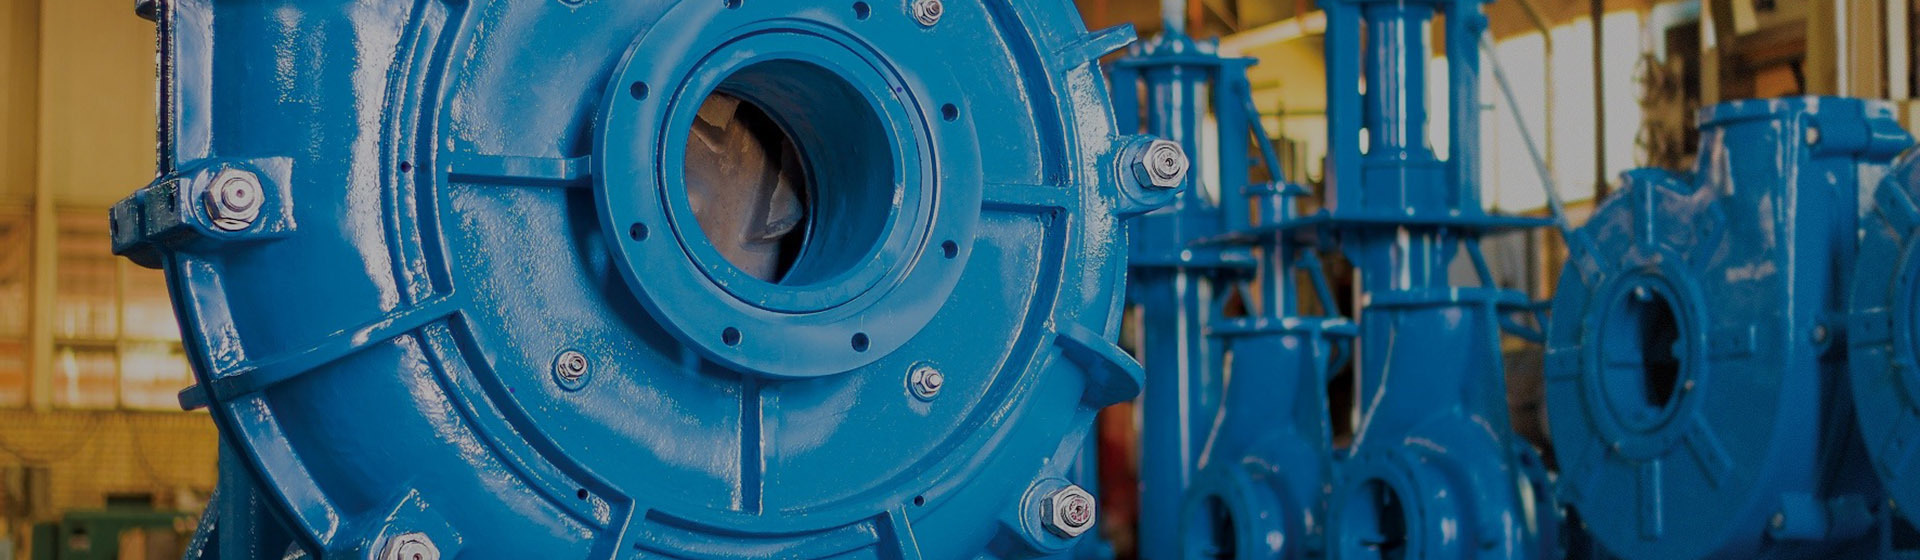
A mud slurry pump is a heavy-duty pump engineered to transport high-concentration mixtures of water, solid particles, and abrasive materials — including mud, sand, gravel, and tailings — through pipelines in demanding industrial environments. Unlike standard centrifugal pumps designed for clean water, a mud slurry pump features reinforced impellers, wear-resistant liners, and enlarged flow passages that allow solid particles to pass without causing rapid internal damage.
The term "slurry pump" is sometimes used interchangeably with mud pump, sludge pump, or sand pump, depending on the industry. In oil and gas drilling, the machine is typically called a mud pump for drilling or high pressure mud pump. In mining and dredging contexts, you will encounter terms like mining slurry pump, hydraulic dredging pump, or abrasive slurry pump. All refer to the same fundamental category of industrial mud pump — each variant optimized for a specific set of operating conditions.
Why does this distinction matter? Because selecting a pump based solely on its name — rather than its engineering specifications — is one of the most common and expensive mistakes in procurement. A dewatering pump handles relatively clean water with low solids content; a true heavy duty slurry pump is built to withstand a solid-liquid mixture weight concentration of up to 45% for mortar and up to 60% for pulp, according to current product engineering data.
For a detailed technical background on pump engineering principles, see this slurry pump overview on Wikipedia.
Main types of mud slurry pumps compared
The right pump type is determined by your application's pressure requirements, solid particle characteristics, and site constraints. Here is a direct breakdown of the five main categories in use across Indonesian mining and construction projects in 2026.
Centrifugal vs. reciprocating: the fundamental split
The majority of slurry transfer pump applications use centrifugal pumps, which rely on a rotating impeller to accelerate slurry outward through a volute casing. They are well-suited for continuous high-volume transfer of abrasive slurry at moderate pressures. Reciprocating pumps — specifically triplex piston or plunger types — generate much higher pressures and are the standard choice for oil and gas drilling mud circulation. Actual testing on site confirms that centrifugal designs dominate where flow volume matters, while reciprocating designs dominate where pressure is the critical variable.
Submersible slurry pump: the site-ready workhorse
A submersible slurry pump operates fully submerged in the slurry, eliminating the need for priming and reducing suction head losses. This makes it the preferred solution for foundation pit dewatering, river dredging, and confined excavation sites common in Indonesian urban construction projects. The integrated motor-pump design also simplifies installation significantly. However, motor cooling depends on the surrounding liquid — running a submersible unit dry even briefly can cause motor burnout.
| Pump type | Typical application | Max solid concentration | Pressure range | Relative maintenance cost |
|---|---|---|---|---|
| Centrifugal slurry pump | Mining tailings, ore processing | Up to 60% (pulp) | Low–medium | Medium |
| Reciprocating triplex pump | Oil & gas drilling mud | Up to 30% | High (up to 350 bar) | High |
| Submersible slurry pump | Pit dewatering, dredging | Up to 45% (mortar) | Low–medium | Low |
| Screw pump | Directional drilling, low-shear transfer | Up to 40% | Medium | Medium |
| Pneumatic diaphragm pump | ATEX zones, intermittent duty | Up to 35% | Low–medium | Low |
How to choose the right mud slurry pump for your project
Choosing a mud slurry pump correctly comes down to four core variables: solid particle size, solid concentration, required head, and flow rate. Get all four right, and your pump runs efficiently for years. Miss even one, and you are looking at premature wear, frequent shutdowns, and inflated operational costs.
Step-by-step selection process
- Define the slurry characteristics: Measure the solid particle size (D50 and D85 values), solid weight concentration (%), and the abrasiveness index of the material. For example, coal tailings in Kalimantan have very different abrasiveness levels compared to silica sand from riverbed dredging in Sumatra.
- Calculate the required head and flow rate: Use the system curve method — account for static head, pipeline friction losses, and any elevation changes. A common mistake is specifying only static head and ignoring friction, which leads to undersized pumps running at damaging off-BEP (Best Efficiency Point) conditions.
- Apply the derating factor: A slurry pump's performance in slurry is always lower than its clear-water performance curve. Apply the HR and QR correction factors based on solid concentration and particle size. Most manufacturers provide derating charts; insist on seeing them before purchasing.
- Select the material of construction: For high-abrasion applications (silica, gravel, ore), specify high-chrome alloy (Cr26 or Cr28) wet-end components. For corrosive and mildly abrasive slurries, natural rubber lining is often more cost-effective and provides better impact resistance.
- Choose the drive configuration: Belt drive allows speed adjustment without replacing the motor — useful when flow requirements change seasonally. Hydraulic variable-frequency drive offers the most precise control and lowest energy consumption but at higher upfront cost.
- Verify series and parallel options: If a single pump cannot meet your head or flow requirements, modern industrial mud pump systems support series installation (to increase head) or parallel installation (to increase flow), giving you operational flexibility.
Why many engineers overlook derating — and pay for it
Why do so many procurement decisions go wrong even when the buyer has done their research? The answer, almost invariably, is that the derating step was skipped. Based on real-world cases in Indonesian nickel mining operations, pumps selected purely from clean-water performance curves routinely deliver only 65–75% of the expected flow when handling actual slurry. This forces sites to run pumps above rated speed, dramatically accelerating impeller and liner wear.
"Slurry pump selection is not simply a matter of matching flow and head — it requires a thorough understanding of the slurry's physical and chemical properties, and the application of appropriate correction factors to the water-performance data. Failure to do so is the single largest cause of premature pump failure in mineral processing applications." — Industry consensus among mining equipment engineers, 2026 regional technical forum.
Key technical specifications explained
Understanding the specification sheet of a heavy duty slurry pump is essential for comparing suppliers fairly. Many vendors present attractive headline numbers that look equivalent on paper but reflect very different real-world performance levels.
Flow rate, head, and efficiency
Flow rate (Q) is measured in m³/h or L/s. Head (H) is expressed in meters. These two values define the pump's operating point. Efficiency (η) tells you what percentage of the motor's input power is actually transferred to the fluid — a critical factor for long-term energy costs. In Indonesia, where industrial electricity tariffs from PLN are calculated per kWh consumed, a pump running at 60% efficiency versus 75% efficiency represents a significant monthly operational cost difference on a continuous-duty application.
Solid handling capacity and liner life
Maximum particle size (in mm) and maximum weight concentration (%) define the pump's solid handling envelope. As noted, this series of slurry pumps supports a maximum weight concentration of 45% for mortar and 60% for pulp — values that cover the vast majority of Indonesian mining and dredging applications. Liner life, typically expressed in operating hours before replacement, varies enormously by material and slurry type. High-chrome alloy liners handling silica sand at high velocity may last 800–1,200 hours; rubber-lined versions handling softer coal tailings can exceed 3,000 hours between replacements.
How to install and operate a mud slurry pump correctly
Even a correctly specified pump will fail prematurely if installed or operated carelessly. The installation phase sets the baseline for everything that follows — alignment, suction conditions, and startup sequence all have direct consequences on service life and reliability.
Installation checklist
- Mount the pump on a rigid, level concrete base or fabricated steel frame. Vibration from an unstable foundation accelerates bearing wear and seal failure faster than almost any other single factor.
- Keep suction pipework as short and straight as possible. Each 90° elbow on the suction side adds equivalent friction loss — minimize bends, and use full-bore gate valves rather than globe valves on the suction line.
- Install a pressure gauge on the discharge flange and a vacuum gauge on the suction flange. These are your primary diagnostic tools during operation.
- Check shaft seal water supply before startup. Mechanical seals and gland packings on slurry pumps require clean seal-flush water to prevent abrasive particles from migrating into the sealing face. Confirm flush water pressure and flow rate meet manufacturer specifications.
- Start the pump with the discharge valve partially closed, then open it gradually once the pump reaches full speed. Never start against a fully closed valve for extended periods, and never run a slurry pump dry — even briefly.
Common operational errors to avoid
The most damaging operational error is running the pump significantly away from its Best Efficiency Point. Operating at very low flow causes recirculation wear inside the casing; operating at very high flow causes cavitation, which sounds like gravel passing through the pump and causes rapid impeller damage. Monitor discharge pressure and flow continuously, and investigate any deviation from baseline readings immediately. A sudden drop in discharge pressure almost always signals impeller wear or air ingestion at the suction.
Maintenance best practices to extend pump life
Maintenance is where operational costs are either controlled or allowed to spiral. A disciplined preventive maintenance programme consistently delivers 30–50% longer component life compared to reactive repair-only approaches — a finding consistent with data from mining operations across Sulawesi and Kalimantan in recent years.
Daily and weekly inspection routines
Check bearing temperature daily — a rise of more than 15°C above ambient is a warning sign. Inspect gland packing for controlled drip leakage (a slow drip is normal and desirable; zero leakage means over-tightening that generates heat). Lubricate bearings according to the manufacturer's schedule; over-greasing is as harmful as under-greasing. Flush suction and discharge pipework at shift end when possible to prevent solids settling and hardening inside the casing during shutdowns.
Scheduled component replacement intervals
Track operating hours meticulously. Impellers and liners should be inspected at 500-hour intervals and replaced at or before the manufacturer's wear limit — do not wait for catastrophic failure. Bearings should be replaced at scheduled intervals regardless of apparent condition, because slurry pump bearings operate under combined radial and axial loads that cause internal fatigue damage that is not visible externally. Mechanical seals should be replaced as a complete set, not individually, because mismatched seal faces accelerate leakage.
Of course, actual replacement intervals will vary based on slurry abrasiveness and duty cycle. These figures serve as a starting baseline — your site-specific data should refine them over time.
2026 trends: smart monitoring and advanced wear materials
The mud slurry pump market is undergoing a meaningful technological shift in 2026. According to recent industry research, the global slurry pump market was valued at approximately USD 3.1 billion and is projected to reach USD 4.7 billion by 2030, growing at a CAGR of around 6.1%. Two developments are driving the premium segment of this growth.
IoT-enabled predictive maintenance
Smart sensors embedded in pump housings now monitor vibration signature, bearing temperature, seal-flush flow rate, and discharge pressure in real time. This data feeds into cloud-based analytics platforms that generate maintenance alerts before failures occur. In practical terms, this means a mining operation in Papua can receive an alert that a specific pump's vibration pattern indicates impeller imbalance — and schedule a planned replacement during the next shift change rather than dealing with an unplanned shutdown that halts an entire processing line. Predictive maintenance has demonstrated non-planned downtime reductions of up to 40% in early Indonesian adopter sites.
High-chrome alloy and rubber liner advances
Material science is the other major frontier. High-chrome iron alloys (Cr26, Cr28) remain the benchmark for handling hard, sharp mineral slurries. However, 2026 data shows that carbide-ceramic composite coatings and enhanced natural rubber formulations are extending liner and impeller life by 30–50% compared to standard materials from five years ago. Just as a car tyre compound determines how many kilometres you get before replacement, the liner material in a slurry pump ultimately determines your cost-per-tonne-pumped. Specifying the correct material is as important as specifying the correct pump size.
Summary: getting your mud slurry pump decision right
A mud slurry pump is not a commodity purchase. The correct choice depends on understanding your slurry's physical properties, applying derating factors to performance data, selecting appropriate wear materials, and committing to a disciplined maintenance programme. In the Indonesian industrial context — where projects span mining in Kalimantan, nickel processing in Sulawesi, and coastal dredging in Java — pump reliability directly determines project profitability. Take the time to specify correctly at the outset. The cost of getting it right is always lower than the cost of getting it wrong.
Frequently asked questions
Q: What is the difference between a mud slurry pump and a regular water pump?
A: A mud slurry pump is built with abrasion-resistant impellers, thicker casings, and enlarged flow passages to handle solid-laden fluids. A standard water pump uses close-tolerance components designed for clean water — introducing even moderate concentrations of solid particles causes rapid wear and failure within hours or days.
Q: What is the maximum solid concentration a slurry pump can handle?
A: Most heavy duty slurry pumps handle up to 45% weight concentration for mortar-type slurries and up to 60% for pulp-type applications. Exceeding these limits causes severe internal wear and requires custom engineering solutions such as pump-in-series configurations or specialized liner materials.
Q: How long do slurry pump impellers and liners typically last?
A: Service life depends heavily on slurry abrasiveness, particle size, and pump speed. High-chrome alloy parts handling silica sand typically last 800–1,200 operating hours. Rubber-lined versions on softer slurries can exceed 3,000 hours. Applying the correct material to your specific slurry is the single most effective way to reduce replacement costs.
Q: Can a slurry pump be used for dewatering applications?
A: Yes, particularly submersible slurry pumps, which are widely used for pit dewatering and sump applications where the water contains suspended solids. However, if the fluid is predominantly clean water with very low solids content, a standard dewatering pump is more energy-efficient and cost-effective for that specific duty.
Q: How do I know when it is time to replace the impeller on my mud pump?
A: The clearest operational indicator is a measurable drop in discharge pressure and flow rate at the same operating speed — typically a 10–15% reduction from the baseline readings taken when the pump was new or recently serviced. Visual inspection during scheduled shutdowns should also show blade thickness approaching the manufacturer's minimum wear limit.
Key words:
PREVIOUS:
Get A Quote
Note: Please leave your email address, our professionals will contact you as soon as possible!
Related Posts

Contact Us
E-mail:
Office Line:
+86 13780213428
Wechat / WhatsApp:
Address:
Shijiazhuang City Luancheng District Xinyuan West Road and Huancheng West Road intersection Tianshan Wanchuang Park 13 production plant No. 13 A
Sales E-mail Ⅰ
Sales E-mail Ⅱ
Wechat/Whatsapp
Free Consultation
We will contact you within one working day. Please pay attention to your email.
Share
Copyright © Shijiazhuang Yongda Pump Co., Ltd.